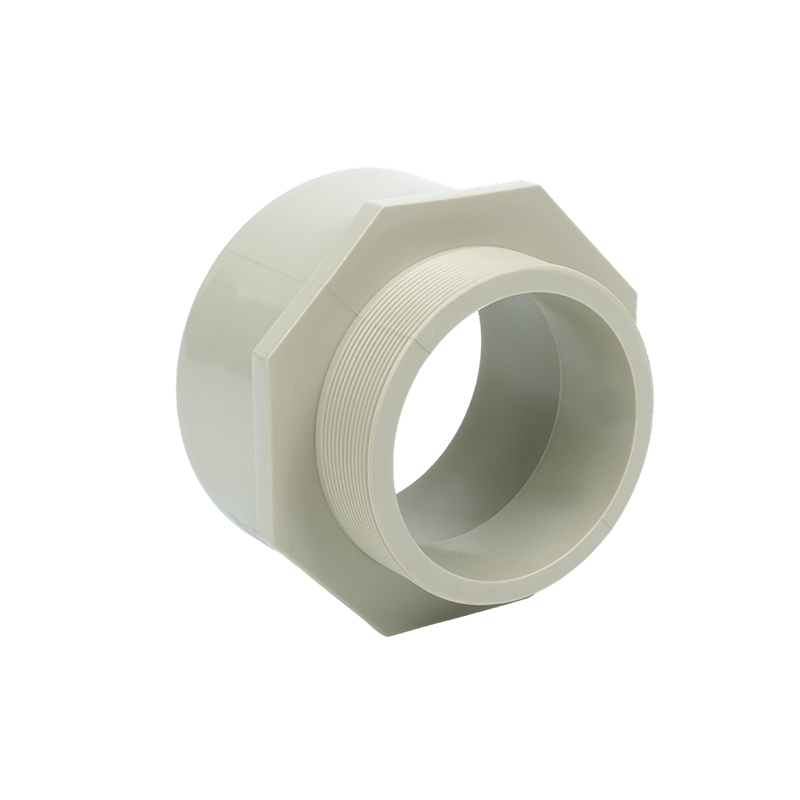
Raccordo per tubo con presa hot melt diretta con dente interno β-Pph 1,0 mpa
1. Installazione veloce e affidabile, conveniente e fa risparmiare tempo; par...
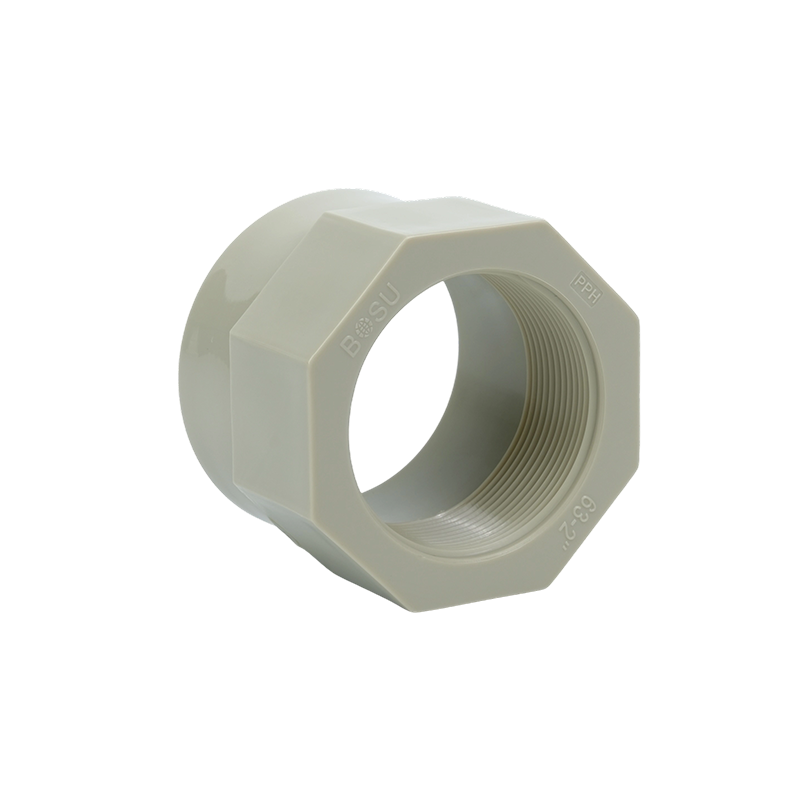
1. Installazione veloce e affidabile, conveniente e fa risparmiare tempo; par...
1. Funzionamento semplice, connessione affidabile, resistenza all'alta p...
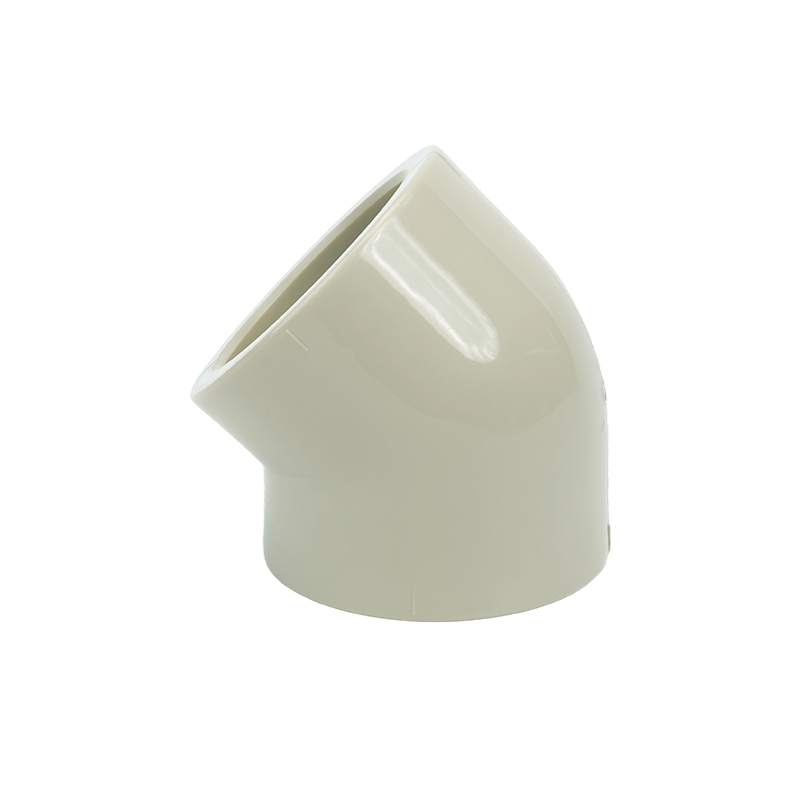
1. Viene utilizzato per collegare i tubi in corrispondenza di una curva e mod...
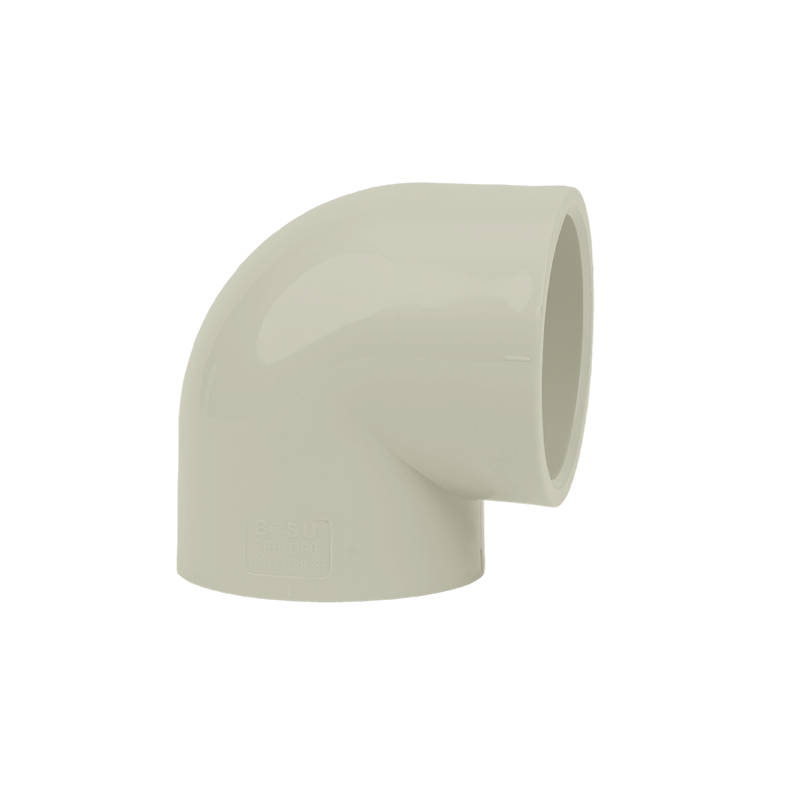
1. Per il collegamento alla curva del tubo, per cambiare la direzione del tub...
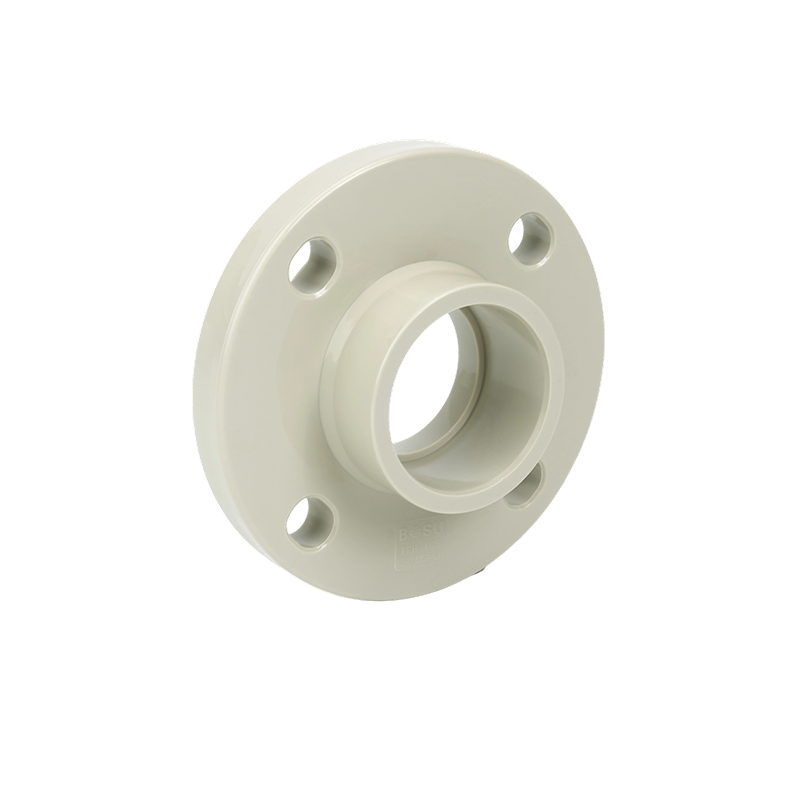
Caratteristiche del prodotto: Facili da installare, questi raccordi ven...
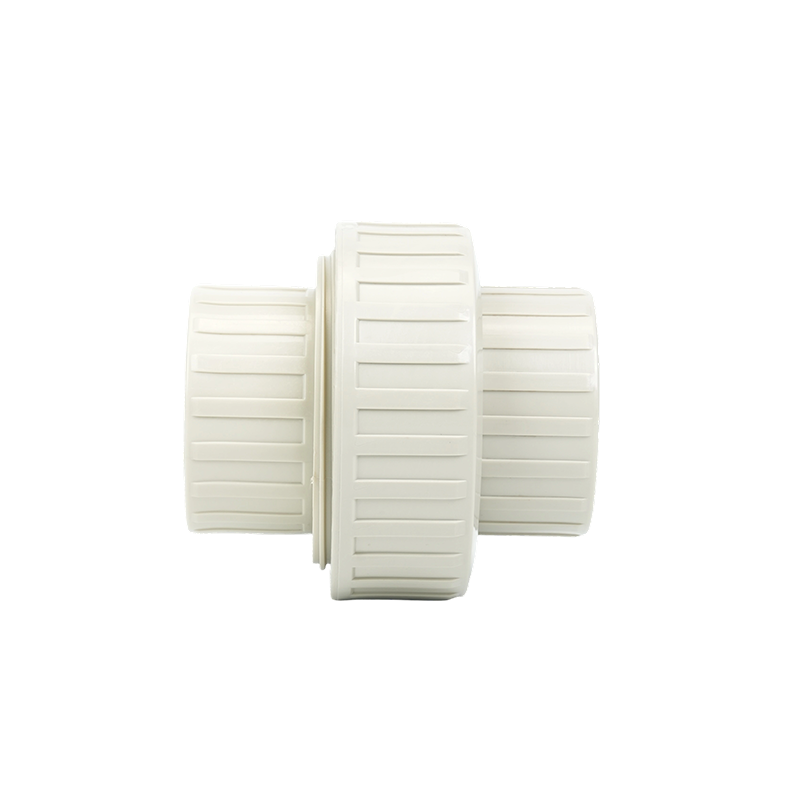
Descrizione: Progettato per il collegamento a tubazioni con estremità filetta...
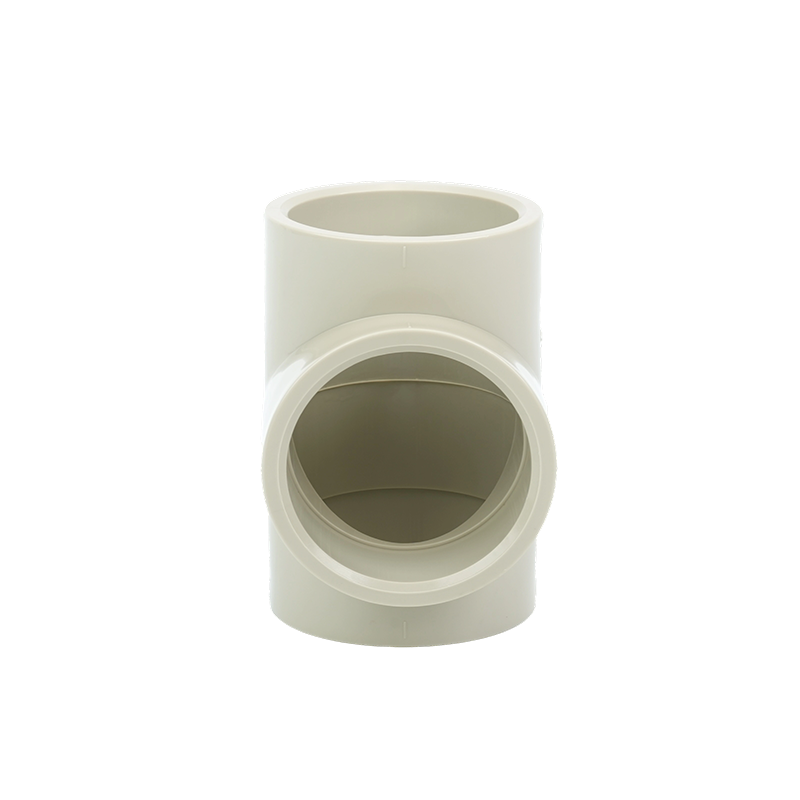
1. Appartiene a uno dei collegamenti del tubo, utilizzato sul tubo di diramaz...
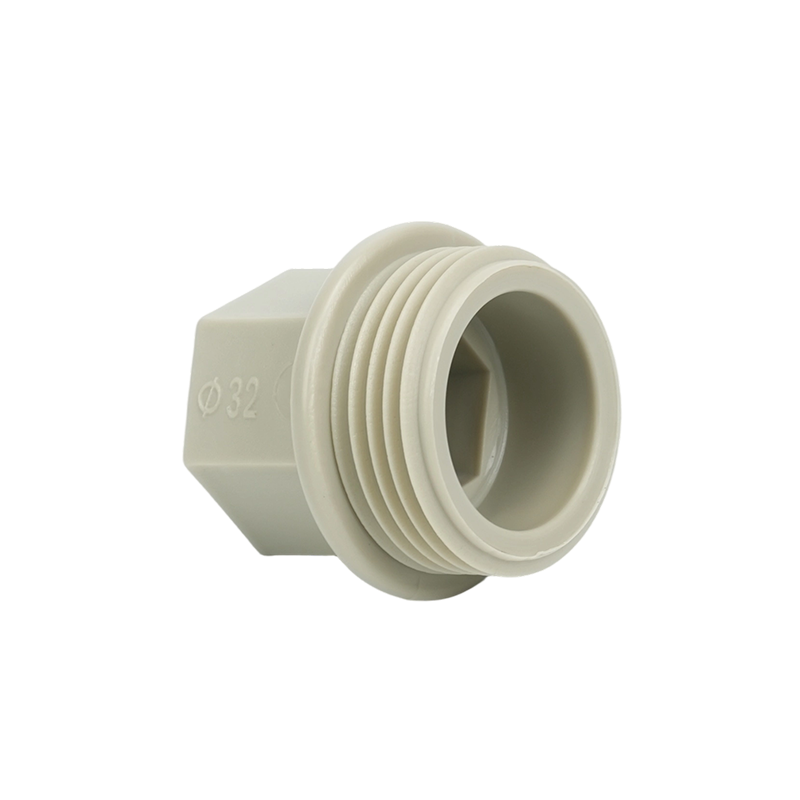
1. Durevole, anticorrosivo, leggero, funziona come una conduttura chiusa, fac...
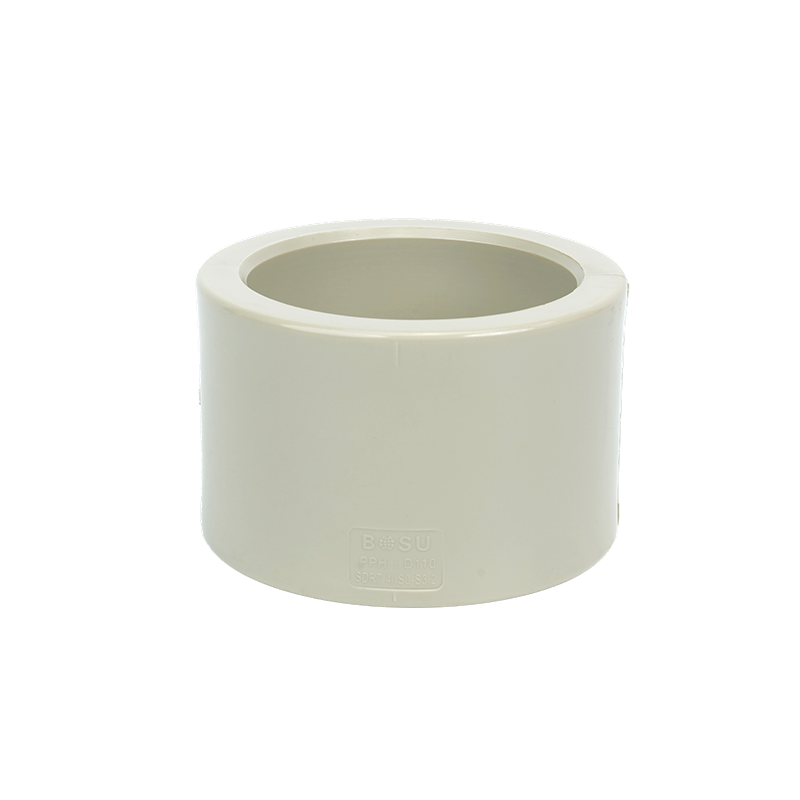
Utilizzato in sistemi di tubazioni che richiedono connessioni a estremità lis...
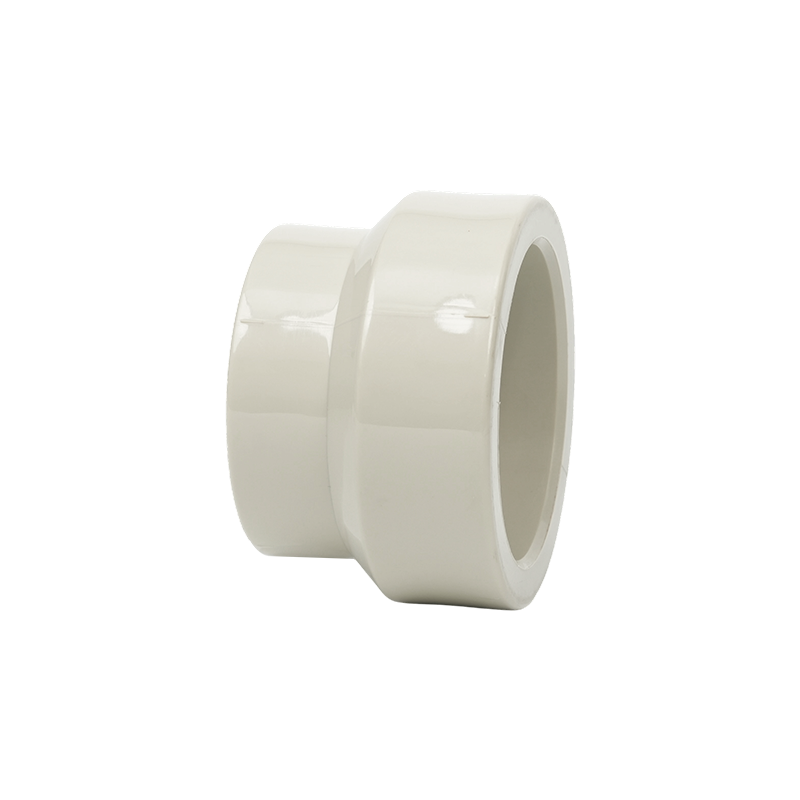
Questo raccordo è progettato per ridurre i disturbi del flusso durante le ...
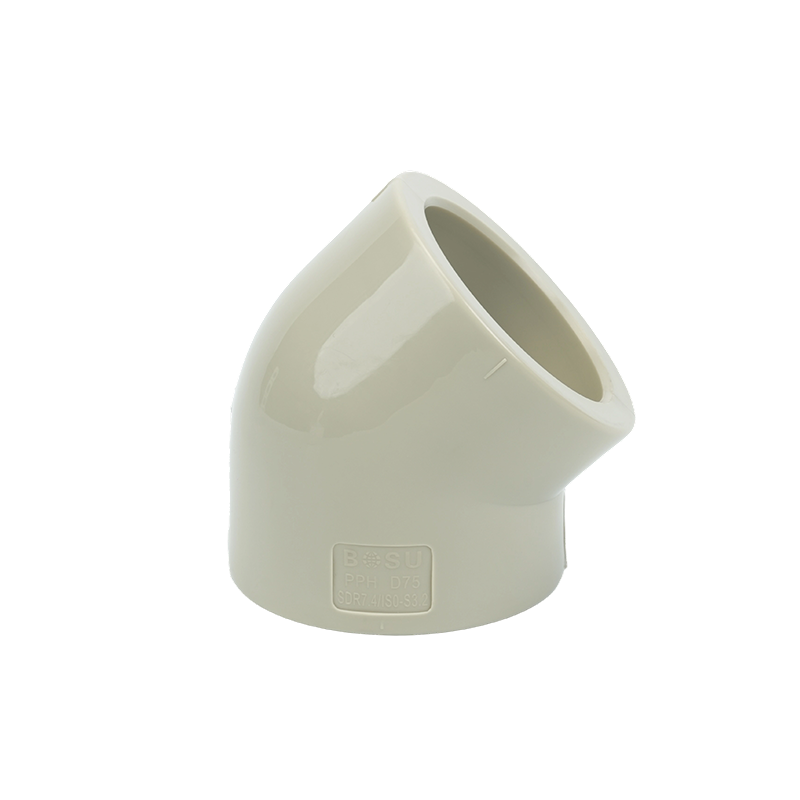
1.Questo raccordo viene utilizzato per modificare la direzione di una tuba...
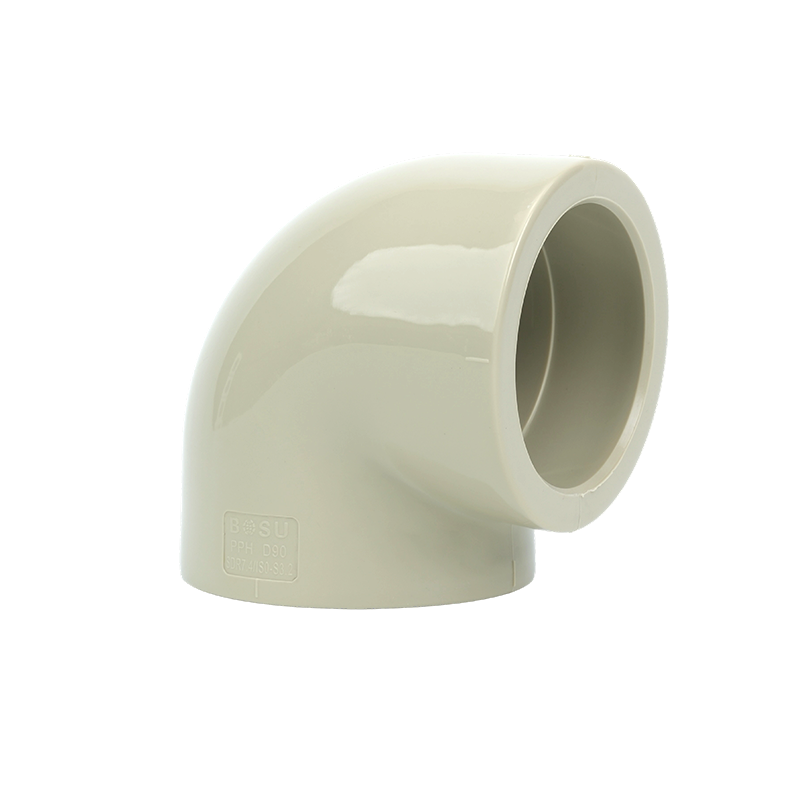
1. Questo raccordo è progettato per cambiamenti direzionali di 90 gradi nelle...
Una squadra di addetti alla chiusura di un impianto chimico aveva ancora un lavoro da fare prima del riavvio: sostituire una guarnizione che perdeva su una valvola dodici metri all'interno di una linea PPH completamente saldata. Tagliare il tubo significava una nuova bobina, una nuova saldatura, un'atte...
Vedi di piùAcquistare una valvola a sfera in plastica chiedendo "le vendi?" è così che i progetti finiscono per pagare due volte. Ciò che in realtà decide se una valvola a sfera in plastica funziona silenziosamente per cinque anni o si guasta nei primi anni, è il materiale del corpo, l'elastomero della guarnizione e il...
Vedi di piùDue installatori, una bobina da 2 tubi in PVDF e una cassa di adattatori flangiati DN 50. Tutto arriva nei tempi previsti e niente si adatta: il tubo misura 60,3 mm all'esterno, mentre l'adattatore è lavorato per un diametro esterno di 50 mm. Nessuna delle due etichette è sbagliata. Le parti appartengon...
Vedi di più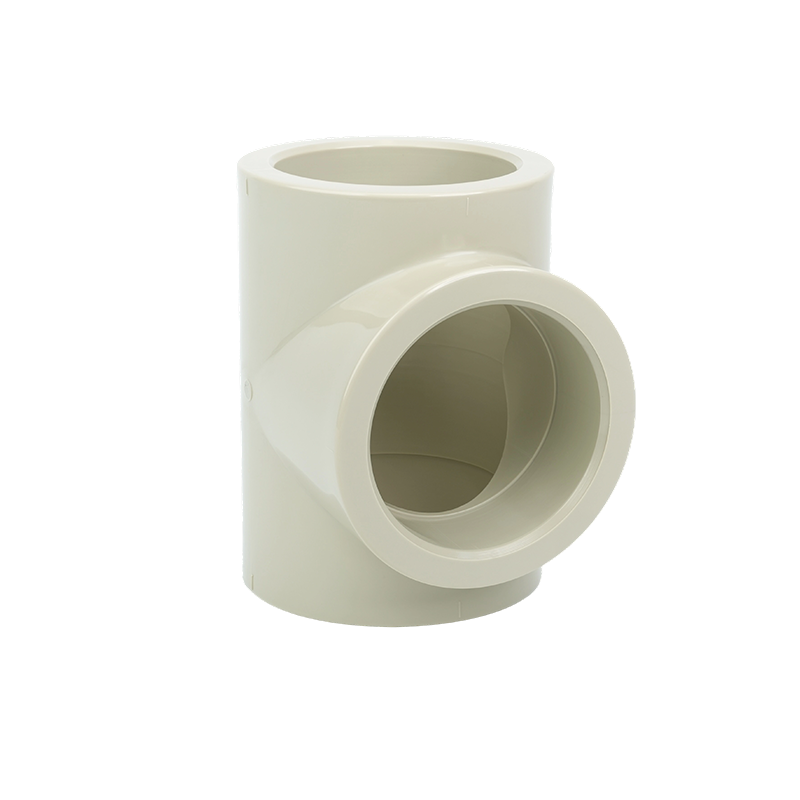
1. È un tipo di raccordo per tubazione, utilizzato dove la tubazione principa...
Vedi di più
Utilizzato in sistemi di tubazioni che richiedono connessioni a estremità lis...
Vedi di più
1. Durevole, anticorrosivo, leggero, funziona come una conduttura chiusa, fac...
Vedi di più
1. Funzionamento semplice, connessione affidabile, resistenza all'alta p...
Vedi di più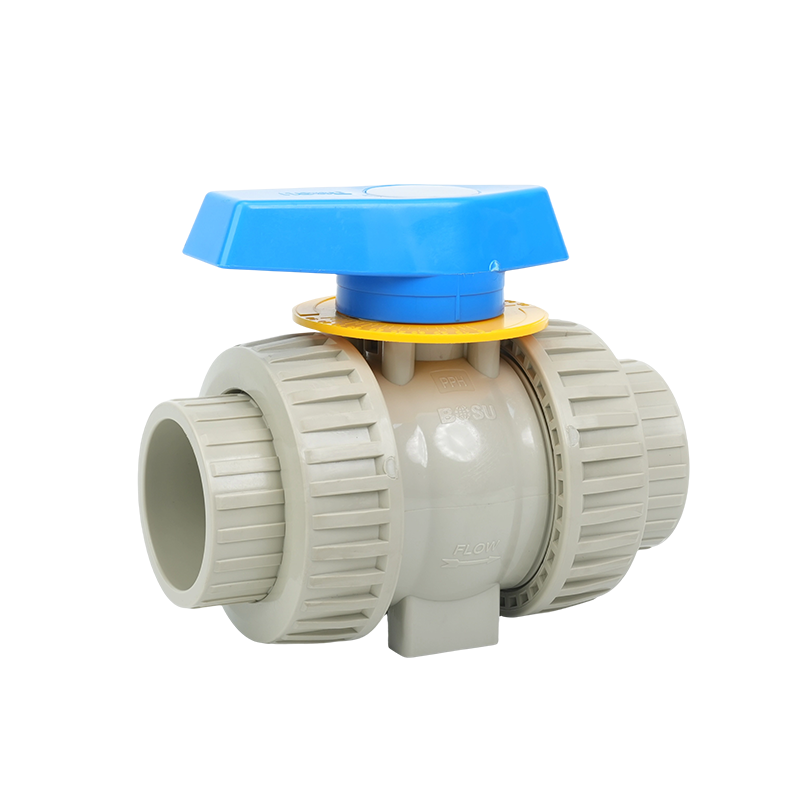
1. Caratteristiche del prodotto: funzione di indicazione della maniglia perso...
Vedi di più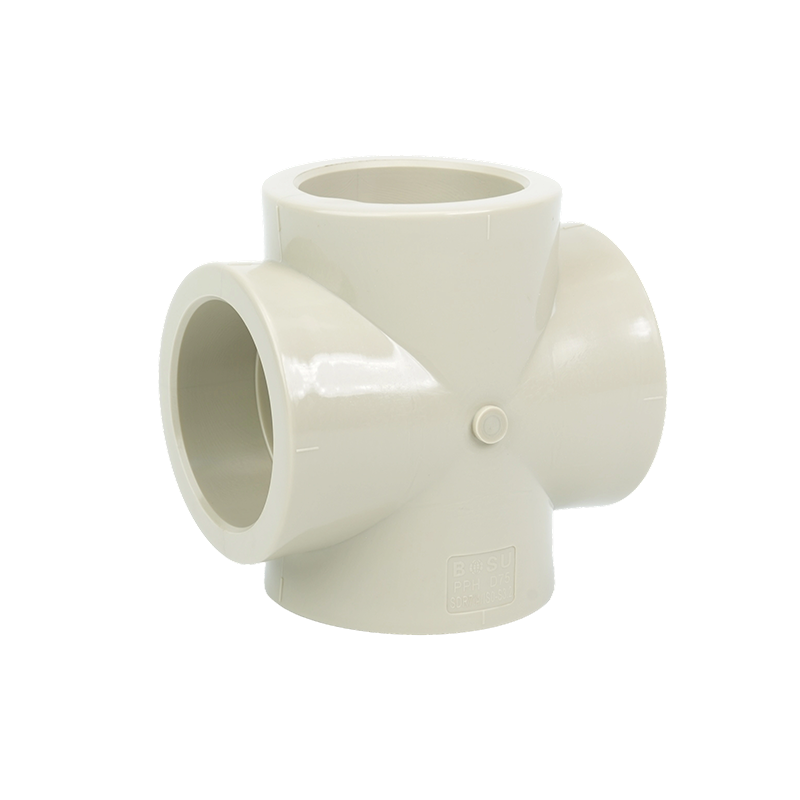
1. Utilizzato per collegare quattro tubi dello stesso diametro che si interse...
Vedi di piùWhat are the key points of installation and welding processes for β-PPH Fittings?
1. Surface Cleaning and Cut Quality
Before installation, oil, dust, and rust must be thoroughly removed from the surfaces of pipes and fittings to ensure a clean contact surface.
Pipe ends must be cut squarely using a specialized cutting tool to ensure a perpendicular, burr-free end face for optimal interlocking strength.
2. Selection of Appropriate Connection Method
For β-PPH materials, two methods can be used: hot-melt welding (electrofusion) or adhesive bonding. Hot-melt welding is the most commonly used process, achieving a leak-free and reliable connection.
3. Key Welding Process Parameters
Heating Temperature: Generally controlled between 210℃ and 230℃ to ensure the material is fully softened without thermal degradation.
Pressure Holding Time: Maintain pressure for 8–12 seconds after heating to allow the melt to fully fill and form a uniform weld.
Cooling: Allow to cool naturally for at least 30 seconds after welding to avoid rapid cooling that could cause internal stress.
4. Quality Inspection and Leak Prevention Measures
After welding, conduct an airtightness test (such as helium leak detection or hydrostatic test) to confirm there are no leaks before putting the pipe into use.
Inspect the weld for bubbles, cracks, or incomplete fusion; re-weld if necessary.
How to select the specifications of β-PPH Fittings based on media type, working pressure, and temperature?
1. Media Corrosivity
For corrosive media such as strong acids and alkalis, thicker wall fittings or corrosion-resistant β-PPH modified materials should be used to resist chemical attack.
For neutral or weakly corrosive media (such as pure water and steam), standard wall thickness fittings can be used.
2. Matching Working Pressure and Temperature
The long-term working temperature range of β-PPH pipes is -20℃ to +100℃, and the short-term maximum withstand temperature is 110℃. Increased temperature significantly reduces pressure resistance; the maximum working pressure (MOP) at 60℃ is approximately 50% of the nominal pressure. When selecting a pipe fitting, the design pressure (usually 1.25 times the highest working pressure) should be considered, along with a temperature correction factor, to ensure that the fitting does not exceed the material's pressure resistance limit under actual operating conditions.
3. Wall Thickness and Nominal Size
Select the appropriate nominal diameter (DN) and wall thickness (PN) based on the viscosity, flow rate, and system pressure drop requirements of the medium.
For high-pressure and low-temperature environments, PN16 and above with thicker walls are recommended; under normal temperature and pressure, PN10–PN12 is sufficient.
4. Influence of Installation Method on Selection
Hot-melt welding has relatively relaxed requirements on pipe wall thickness, but welding quality must be ensured; flange connections have higher requirements on pipe wall thickness and require matching with appropriate flange thickness and bolt specifications.
Prodotti
Informazioni sull'azienda
Indirizzo: N. 55 Haichuan Road, zona high-tech, città di Dongtai, provincia di Jiangsu, Cina
Cellulare: +86 137 7009 5258
Tel: +86-515-85479999
Email: [email protected]
Ci piacerebbe sentire la tua opinione!